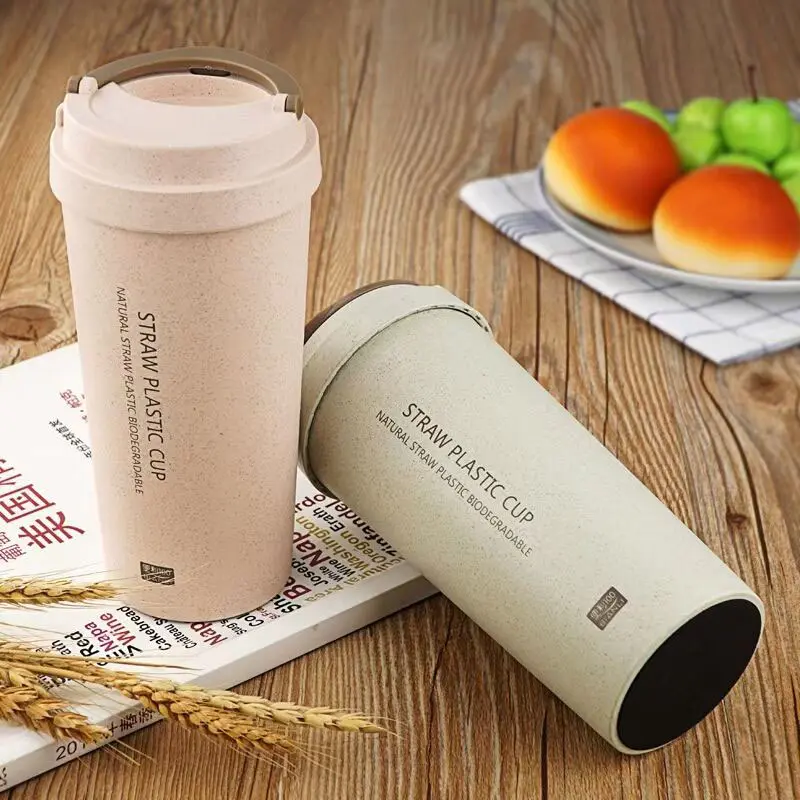
Can lab‑certified straw bio‑based compounds sustain consistent behaviour across real‑world injection‑moulding campaigns?
Bio‑Based builds multi‑layer pre‑validation workflows for Straw Bio-Based Plastic compounds, combining pellet‑batch fibre‑distribution auditing, simulated full‑scale injection‑shear testing and lot‑wise biomass‑content traceability, identifying lab‑hidden material‑behaviour risks ahead of converter mass‑production deployments.
1. Multi‑point pellet‑batch fibre‑distribution auditing avoids intra‑lot property fluctuation
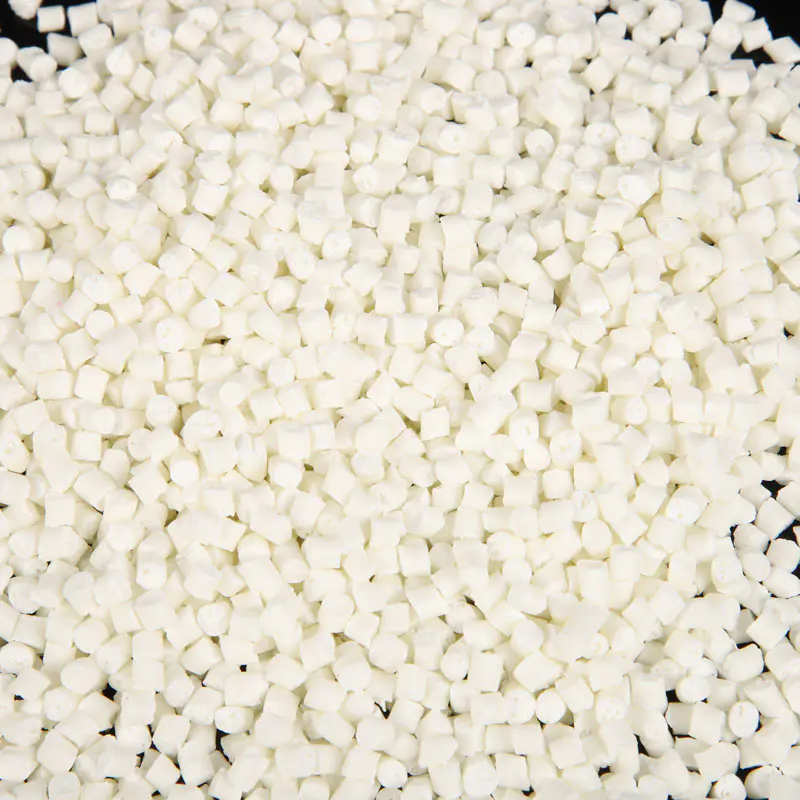
Lab test specimens get taken from well‑mixed small‑quantity reference samples. During continuous compounding manufacturing, poor straw‑fibre screening or insufficient twin‑screw homogenisation creates uneven fibre dispersion within bulk pellet batches. Even though overall batch‑average biomass percentage meets contractual targets, local fibre‑rich and fibre‑lean micro‑zones exist across pellets. After injection‑moulding, this generates random part‑to‑part variance in impact‑resistance and surface texture, which cannot be predicted from single‑point lab‑pellet testing. Bio‑Based extracts multiple grab‑samples from finished bulk lots for microscopic fibre‑distribution assessment. Acceptance thresholds restrict uneven fibre‑agglomeration, stabilising part‑to‑part consistency for downstream consumer‑goods injection‑moulding cycles.
2. Simulated injection‑shear ageing uncovers fibre‑length degradation risks under real‑processing conditions
Material datasheet mechanical values derive from compression‑moulded lab test bars, without experiencing high screw‑shear forces of commercial injection equipment. Under long‑run high‑speed moulding, straw plant fibres undergo shear‑induced break‑down inside the barrel. Effective fibre length shortens progressively, weakening final‑part impact performance even when incoming raw‑pellet testing remains compliant. Many compound suppliers skip shear‑history simulation and only test as‑produced pellets, ignoring property loss triggered by customer‑side processing. Bio‑Based runs simulated twin‑screw shear‑history lab trials replicating typical converter machine parameters. Post‑shear mechanical‑property measurement sets realistic performance expectations, preventing unexpected field‑part brittleness after high‑volume moulding campaigns.
3. Controlled moisture‑absorption characterisation mitigates batch‑dependent moulding‑defect outbreaks
Straw‑derived bio‑based pellets are inherently hygroscopic. Lab‑test pellets stay stored under strictly controlled low‑humidity conditions. In real‑world industrial warehouses and sea‑freight containers, bulk material absorbs variable ambient moisture. If converters apply generic drying settings sourced from datasheets, variable residual‑moisture creates intermittent surface blistering, splay marks and internal voids on finished components. Defect rates jump and fall unpredictably lot‑by‑lot, hard to attribute to either compound quality or converter equipment. Bio‑Based performs humidity‑exposure ageing for each formulation grade, documenting moisture‑uptake curves and application‑specific drying‑parameter guidance. These practical processing recommendations get delivered alongside each shipment, lowering sporadic mould‑defect occurrence for downstream manufacturing partners.
4. Lot‑linked biomass‑content verification meets global eco‑claim audit requirements
Many sustainable‑brand customers must substantiate public biomass‑content marketing claims for retail‑market regulators and third‑party eco‑auditors. Generic datasheet nominal‑values cannot replace actual measured lot‑specific biomass figures. Single prototype‑batch test‑reports hold no validity for successive mass‑production lots. Without batch‑by‑lot measured‑value documentation, finished consumer‑goods risk eco‑claim challenge, marketplace listing‑restriction or import‑customs hold‑up. Bio‑Based carries out lot‑specific biomass‑content testing for every straw bio‑based plastic production run. Complete English‑language measured‑result archives accompany bulk‑pellet shipments, supporting downstream brand‑owners for regulatory eco‑claim verification without extra third‑party lab expense.
5. Thermal‑history stability mapping prevents discoloration drift over extended barrel residence‑time
Short‑duration lab compound testing does not replicate occasional production interruptions. When injection‑moulding lines pause for tool‑maintenance, bio‑based material remains sitting inside hot screw‑barrels for extended residence‑time. Straw‑fibre components are susceptible to thermal‑oxidative discoloration under prolonged high‑heat exposure. This yields scattered yellow‑brown discoloured parts interspersed within otherwise normal‑looking production batches. Such defects only surface on‑customer‑shop‑floor and are absent from fresh lab‑pellet evaluations. Bio‑Based executes variable residence‑time thermal‑exposure lab assessment for each straw‑compound grade. Colour‑shift threshold data informs converter operating‑guidance, reducing random discoloration‑scrap risk during real‑world interrupted‑production scenarios.
6. Formulation‑specific compatibility review flags secondary‑material interaction risks ahead of product design freeze
Product‑design teams often select straw bio‑based compound and then pair it with colour‑masterbatches, release‑agents or post‑mould surface‑coatings without pre‑testing full‑system compatibility. Certain additives interact chemically with straw‑fibre components, triggering accelerated ageing, surface blooming or unexpected odour generation in finished goods. These incompatibilities rarely emerge during simple pellet‑only lab characterisation. Bio‑Based provides pre‑project formulation‑compatibility assessment upon receipt of customer master‑batch and auxiliary‑material samples. Potential adverse interactions get identified in advance, avoiding costly late‑stage mould‑tooling modification after product‑tool investment has already taken place.
Related News
- What Multi-Scenario Tunable Bio-Based Plastics Help Brands Pass Global Plastic Regulatory Audits?
- How Is Sustainable Bio-based Plastic Reshaping the Future of Materials?
- Why Is Biodegradable Plastic Becoming Essential for Modern Industry?
- What Makes Starch-Based Plastic the Future of Sustainable Materials?
- What Makes Straw Fiber Plastic the Future of Eco-Friendly Materials?
- What Makes Bamboo Fiber Plastic the Future of Sustainable Material Innovation?
Leave me a message